About Redler Chain Conveyor
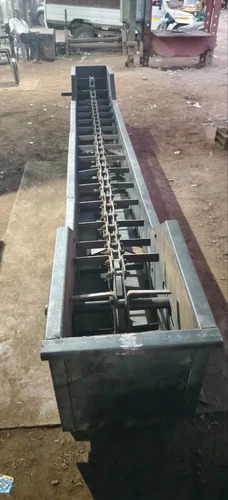
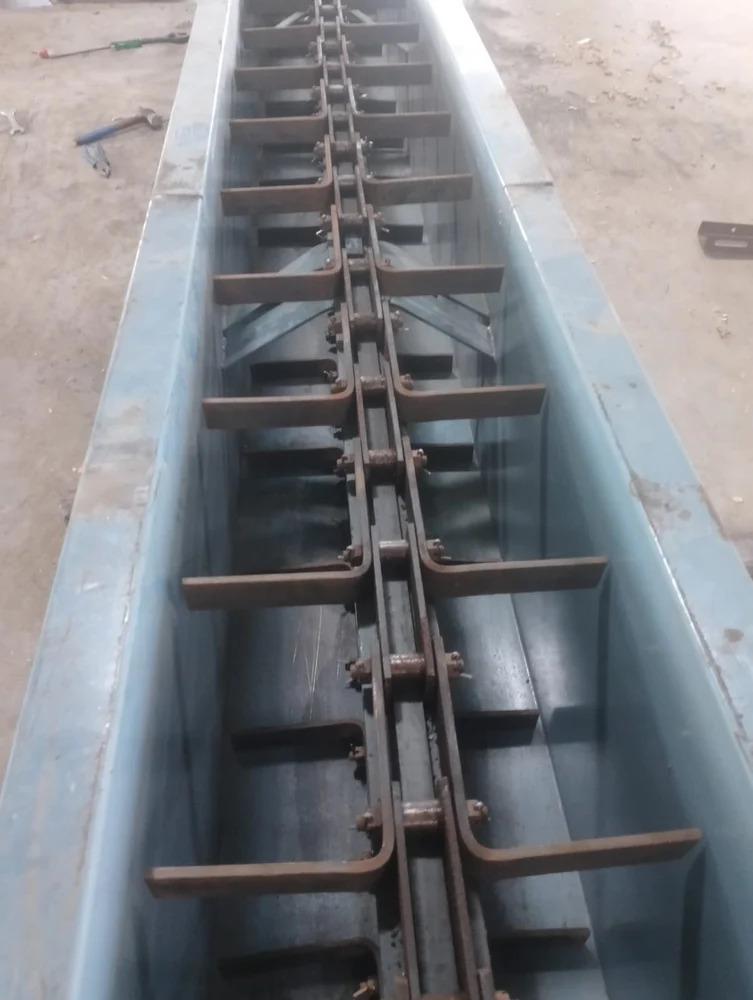
Grab yours now and elevate your productivity with the Redler Chain Conveyor, a popular solution trusted by manufacturers and suppliers across India. This astounding machine, with a pitch of 250 mm and a conveyor width of 400 mm, offers inestimable efficiency for fly ash and fertilizer handling. Featuring a fully enclosed, corrosion-resistant structure, heavy-duty sprockets, and a robust 22 mm hardened steel chain, it ensures ravishing durability and low maintenance. Powered by an automatic electric motor and capable of 5 TPH load, the Redler Chain Conveyor is designed to deliver premium performance, every time.
Key Features and Application of Redler Chain Conveyor
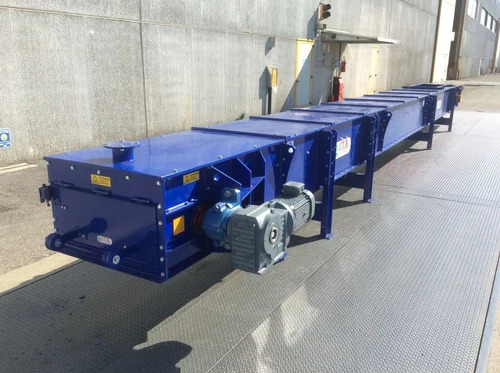
The Redler Chain Conveyor boasts an enclosed rectangular trough, sturdy bolted flights, and heavy-duty, corrosion-resistant components for unparalleled reliability. Its variable speed, low maintenance requirements, and automatic control make it ideal for handling materials such as fly ash and fertilizer. The conveyor can be deployed horizontally or vertically, offering flexibility for various industrial setups. Its fully enclosed design ensures dust-free operation, while effortless adjustment of speed and flight type offers customized application across different environments.
Sample Policy, Packaging and Delivery of Redler Chain Conveyor
We offer a customer-oriented sample policy to help you evaluate the premium quality of our Redler Chain Conveyor. Each unit is meticulously packaged for safe shipment, conforming to domestic and export market standards. Our robust packaging practices safeguard your investment during transport. Delivery times are optimized for quick response, ensuring your conveyor arrives in perfect condition, ready for immediate installation and operation. Experience reliable shipment processes and uncompromised quality with Redler conveyors.
FAQ's of Redler Chain Conveyor:
Q: How does the Redler Chain Conveyor ensure low maintenance operation?
A: The Redler Chain Conveyor features a fully enclosed, corrosion-resistant structure and a heavy-duty chain design, which minimizes wear and reduces maintenance needs for sustained, efficient operation.
Q: What materials are suitable for handling with this conveyor?
A: The conveyor is engineered primarily for the safe and efficient transportation of fly ash and fertilizers, but it can also accommodate similar free-flowing or granulated materials in industrial settings.
Q: When can I expect the delivery once my order is placed?
A: Upon order confirmation, delivery times are scheduled for prompt shipment, with timelines varying based on order size and location, ensuring your equipment reaches you without unnecessary delay.
Q: Where can the Redler Chain Conveyor be installed in industrial settings?
A: It is versatile and suitable for installation in fertilizer plants, power stations, and material handling units dealing with fly ash, thanks to its ability to function in both horizontal and vertical arrangements.
Q: What are the benefits of using a fully enclosed Redler Chain Conveyor?
A: A fully enclosed design provides dust-free operation, protects the conveyed material from environmental contamination, and contributes to a cleaner, safer workplace.



 Send Inquiry

 Send Inquiry
 Send Inquiry
 Send SMS


