About Bucket Elevator Conveyor
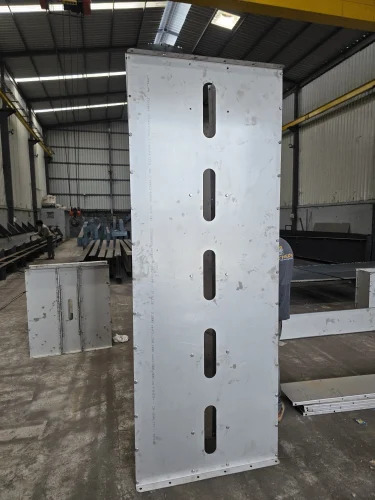
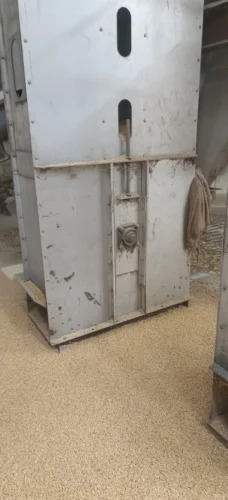
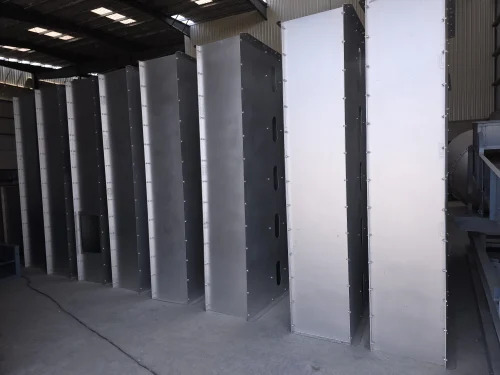
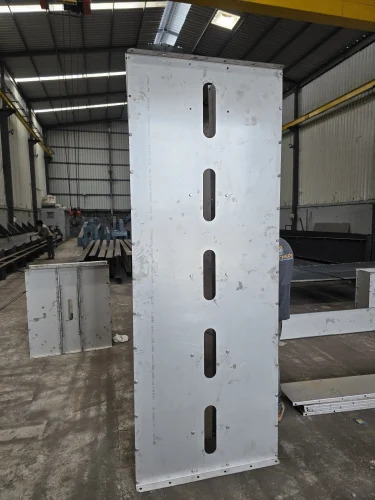
Ending Soon: Find your splendiferous solution for vertical transport with our Ultimate Bucket Elevator Conveyor! Specially designed for factory floors, this robust conveyor boasts a fully decorated SS304 frame and buckets, ensuring stellar corrosion resistance and longevity. Grab this manually operated equipment featuring a sealed slot enclosure, close bucket pitch, and high customization. With a substantial 5 TPH load capacity and 3L bucket volume, it's ideal for rice mills, food processing, cement, mining, and more. Don't miss out on this precision-crafted, highly durable industrial marvel!
Ultimate Performance and Competitive Advantages
The Bucket Elevator Conveyor sets itself apart with its corrosion-resistant SS304 structure and close-spaced buckets, which offer maximum efficiency for tough industrial demands. Suitable for handling rice, cement, chemicals, grains, minerals, and fertilizers, this equipment stands as an ultimate choice for a wide variety of application media. Additional features include its sealed slot enclosure for dust control, high load capacity, and custom design, making it a splendiferous solution for many industrial environments.
Sample Availability, Packaging Details, and Delivery
Sample units of this decorated Bucket Elevator Conveyor can be provided on charge with a formal purchase order. Each shipment is thoroughly packaged with premium materials to safeguard the elevator throughout transit. Once your order is confirmed, expect prompt handling-delivery time typically ranges from a few days to a couple of weeks depending on customization. Trust us to manage your order from purchase to final shipment, ensuring a seamless supply process for every factory floor.
FAQ's of Bucket Elevator Conveyor:
Q: How does the Bucket Elevator Conveyor benefit industrial operations?
A: This conveyor ensures efficient and reliable vertical transport for materials, minimizing downtime and increasing productivity in various industries, including food processing, cement, chemicals, and grain handling.
Q: What materials can be handled by the Bucket Elevator Conveyor?
A: The conveyor is suitable for a wide range of application media such as rice, flour, cement, chemicals, grains, fertilizers, and minerals, making it exceptionally versatile.
Q: Where can the Bucket Elevator Conveyor be installed?
A: Designed for indoor installation on factory floors, its sealed slots ensure dust-free operation and minimal material spillage within industrial environments.
Q: What process is involved in placing an order and receiving a sample?
A: You can request a sample unit on charge by submitting a formal purchase order. Once processed, the unit is securely packaged and swiftly shipped to your location.
Q: When can I expect delivery after making a purchase order?
A: Delivery times typically range from a few days to a couple of weeks depending on the level of customization required for your conveyor unit.
Q: How is the Bucket Elevator Conveyor maintained for longevity?
A: With its SS304 stainless steel construction and close-spaced buckets, the conveyor is built for durability and requires minimal ongoing maintenance under standard industrial conditions.



 Send Inquiry

 Send Inquiry
 Send Inquiry
 Send SMS


